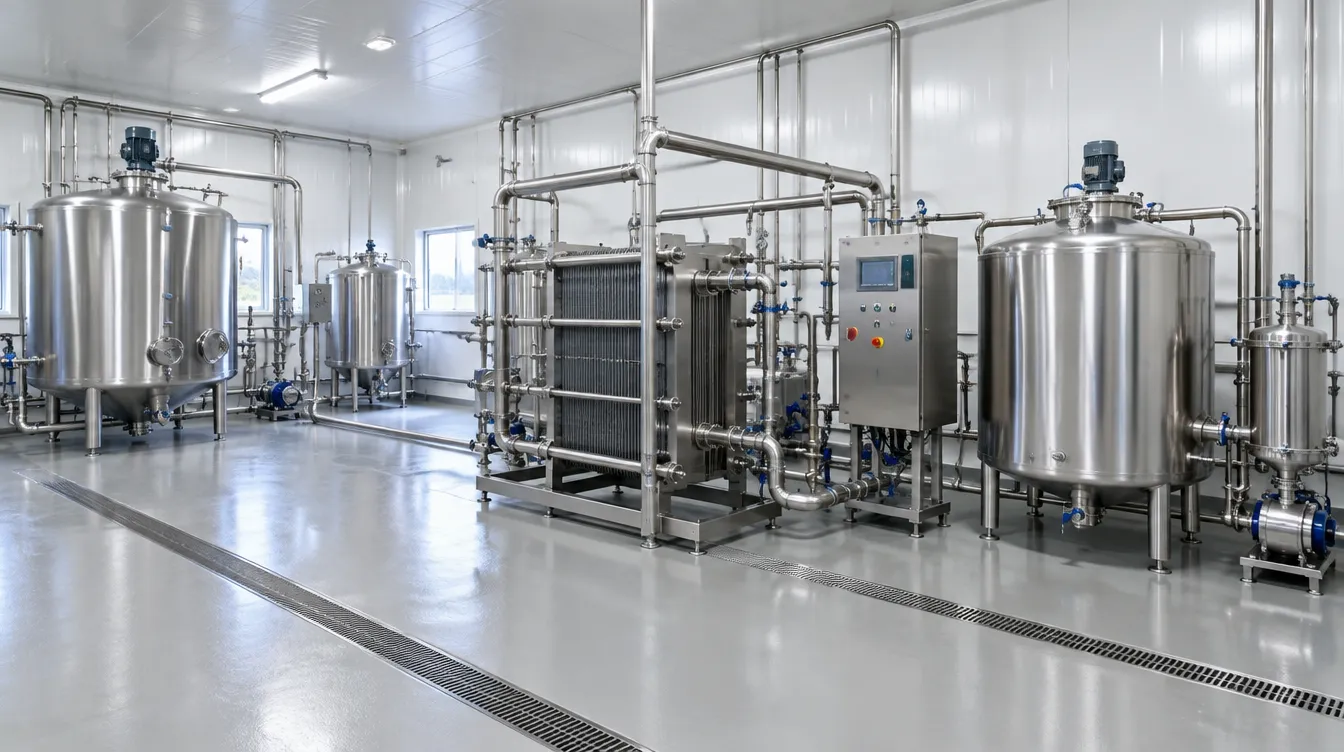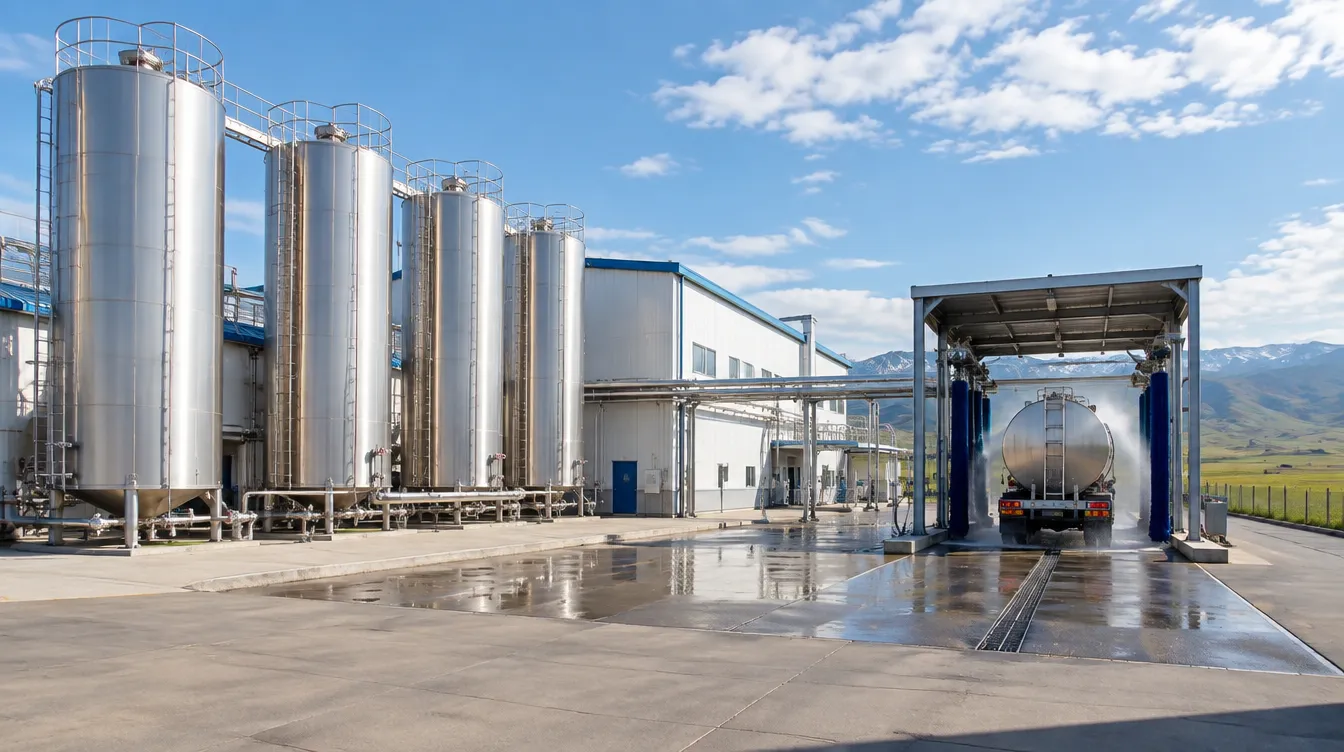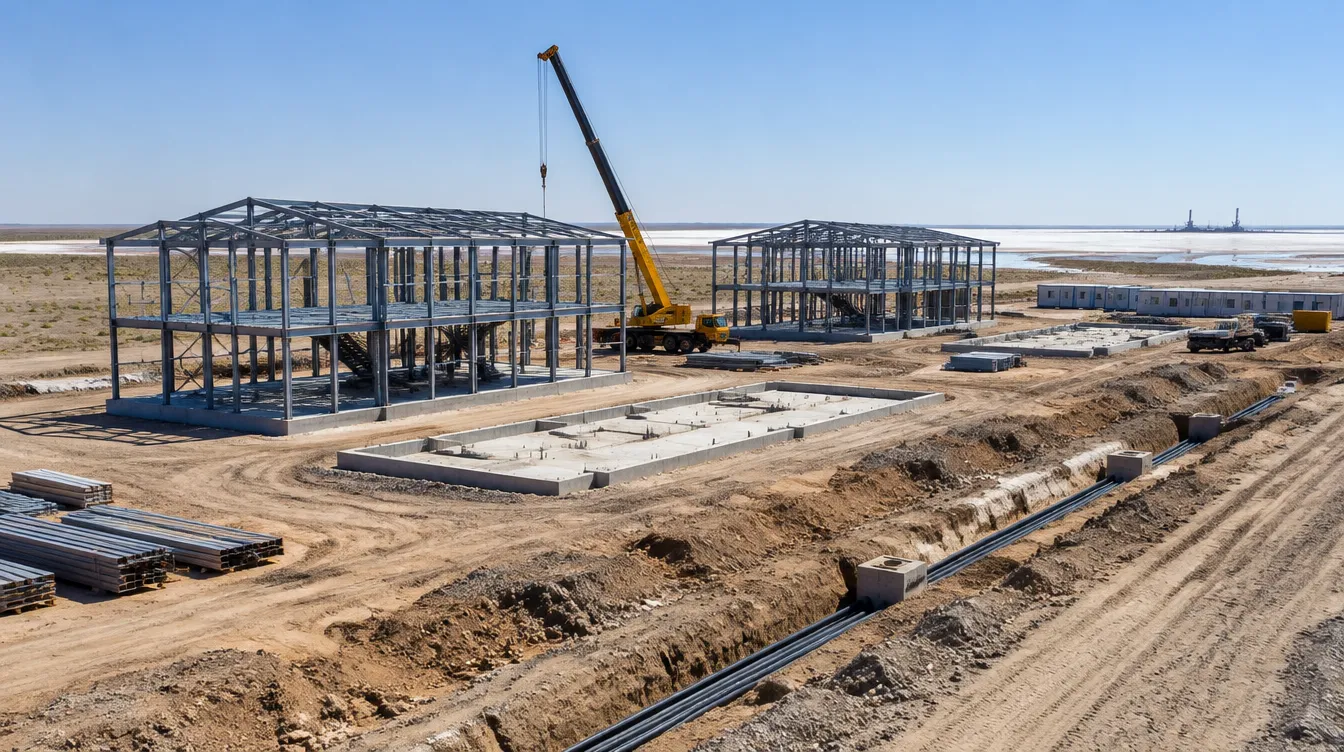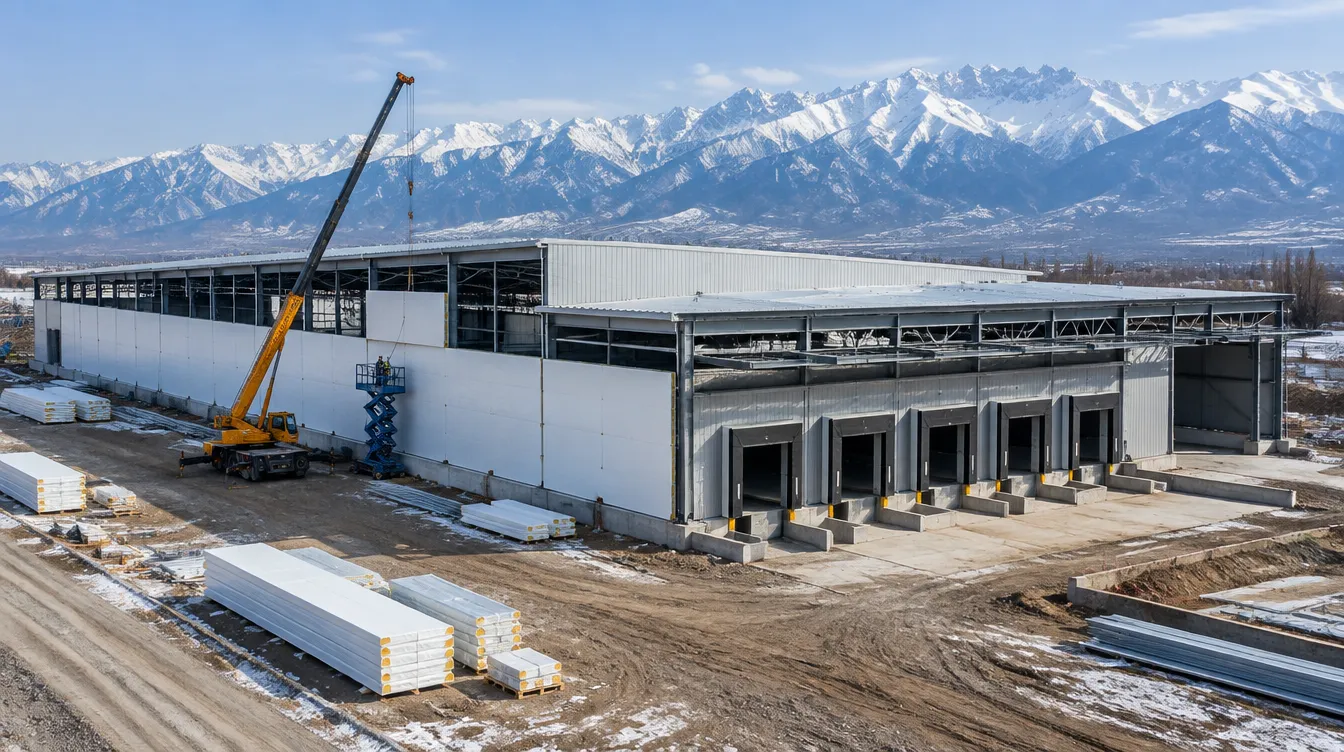
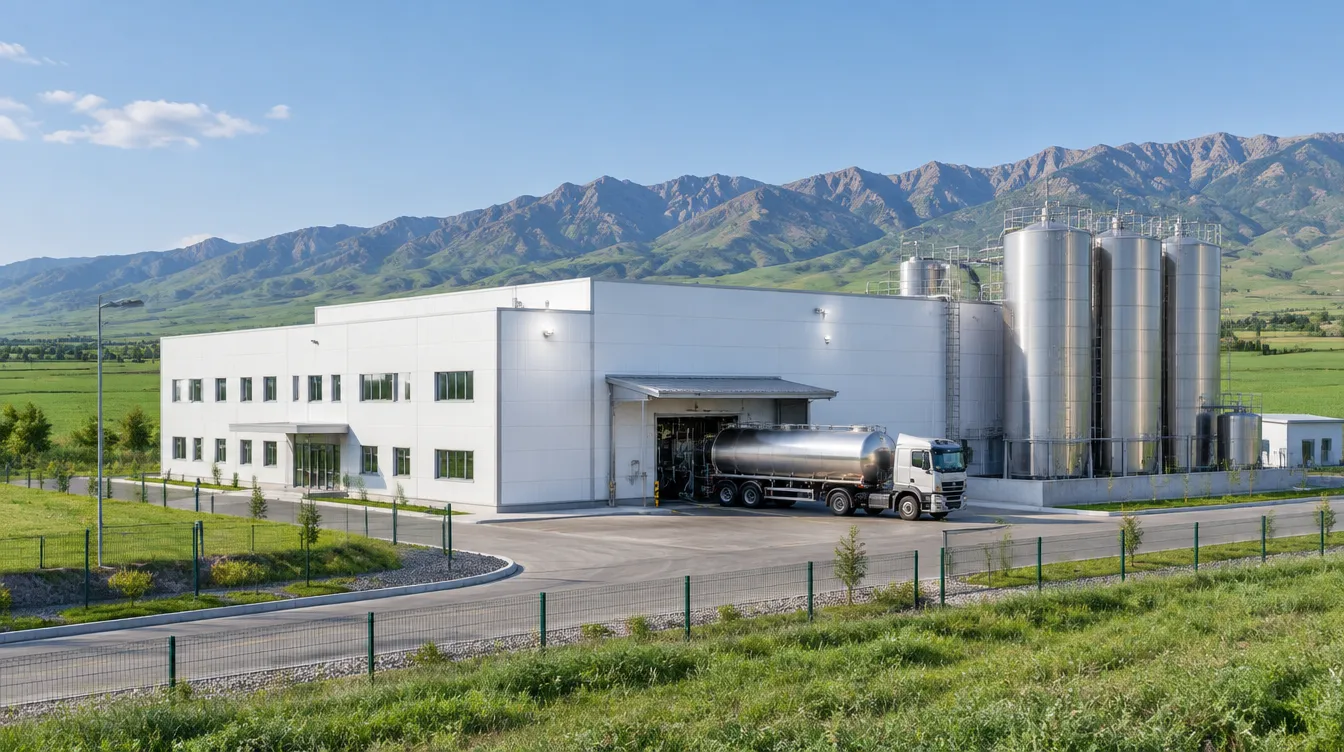
The new plant enabled the agricultural company to process milk from its own and neighbouring farms on site, producing pasteurised milk, kefir and cottage cheese. Construction was delivered on a turnkey basis in compliance with sanitary requirements for food production.
Work completed
- steel frame clad with food-grade coated sandwich panels;
- resin floors sloping to stainless steel drains;
- separation into clean and dirty zones, hygiene locks for staff;
- reception area with a milk tanker wash bay;
- cold rooms at +2…+6 °C, a boiler house and on-site wastewater treatment.
Outcome
The plant was commissioned two months ahead of schedule. The supplier's process equipment was installed in parallel with finishing works, which shortened commissioning time.